NTI Repel™ brings hydrophobic, oleophobic and electronics protection coatings into one portfolio for textiles, leather, polymers, metals and PCBA, with PFAS-free options available across the product range
Market access, user expectations, smarter connected products and new material systems are raising the performance expected from repellent surfaces across consumer, electronics, automotive and industrial applications
PFAS restrictions, certification limits and restricted substance requirements are moving repellency chemistry into sourcing and qualification decisions earlier, especially for textiles, leather, footwear and consumer products sold across multiple markets
Consumers increasingly expect premium products to stay cleaner, easier to maintain and pleasant to touch through repeated use, making stain release, fingerprint control, smooth touch and preserved appearance part of perceived product quality
AI enabled electronics, wearables, connected vehicles and sensor rich devices are adding more display, camera, glass and touch interfaces where oil, sebum and moisture must be controlled without compromising optics, touch response or sensing
Engineered textiles, lightweight polymers, composites, curved cover glass and coated metals require different chemistry, deposition and validation routes, making application specific surface design more important than a single generic repellency specification
PFAS requirements are moving from policy into product specifications. From 10 October 2026, EU REACH limits on PFHxA and related substances apply to specified consumer textiles, leather, accessories and footwear, while broader PFAS restrictions and customer restricted substance lists continue to evolve. NTI Repel™ provides PFAS-free options across NTI Hydro Repel™, NTI Oleo Repel™ and NTI Electro Repel™ to support earlier material selection and qualification.
PFAS is a broad family of fluorinated chemicals that includes substances such as PFOA and PFOS. As regulation and customer requirements expand beyond individual legacy substances, repellency chemistry is increasingly becoming part of material selection, supplier qualification and market access.
NTI develops PFAS-free options for water and stain repellency, anti fingerprint and easy clean surfaces, and electronics moisture and corrosion protection. Each route is selected and qualified around the actual material and end use, so PFAS requirements can be addressed together with the durability, appearance, touch or electrical performance expected from the product.
Regulatory reference: Commission Regulation (EU) 2024/2462 amending REACH introduces PFHxA limits for specified consumer textiles, leather, related accessories and footwear from 10 October 2026.
NTI Advanced PECVD combines high density plasma with dry vapor phase thin film formation to engineer functional protection directly at the surface. Greater process control helps tune repellency, moisture protection and durability across fabrics, polymers, metals and selected electronic assemblies while minimizing coating build
Form the functional layer in the vapor phase, avoiding sprayed or dipped coating add on and separate liquid drying or cure steps that can influence feel, appearance, dimensions or production flow
Higher density plasma provides greater control over activation and film formation across flexible textiles, polymers, metals and selected electronic assemblies, allowing the process window to be matched to the substrate and use condition
Greater process control provides more room to balance wetting behaviour, abrasion retention and coating consistency, then carry qualified conditions into recurring production
NTI Advanced PECVD creates functional protection directly at the surface, giving greater control over repellency, durability and coating performance while helping preserve the feel, finish, geometry and integration of the finished product
Representative comparative values illustrate PECVD and plasma polymerization performance under specific material, chemistry and test conditions. They are technology benchmarks and do not represent universal NTI product specifications. Final coating performance is confirmed for the selected material, coating configuration and application requirements.
Whatever the surface challenge, NTI Repel™ is designed to connect the protection need with the right material route. Answer two simple questions and the finder will identify the most relevant starting point, including complementary routes when more than one surface function matters
Each NTI Repel™ product is organized around the surface function, compatible material class and performance measures customers commonly use to evaluate the coating in their application
NTI combines coating characterization and application testing to verify wetting, water resistance, oil and stain release, durability, corrosion, optical quality, surface feel and chemistry against agreed product requirements before production
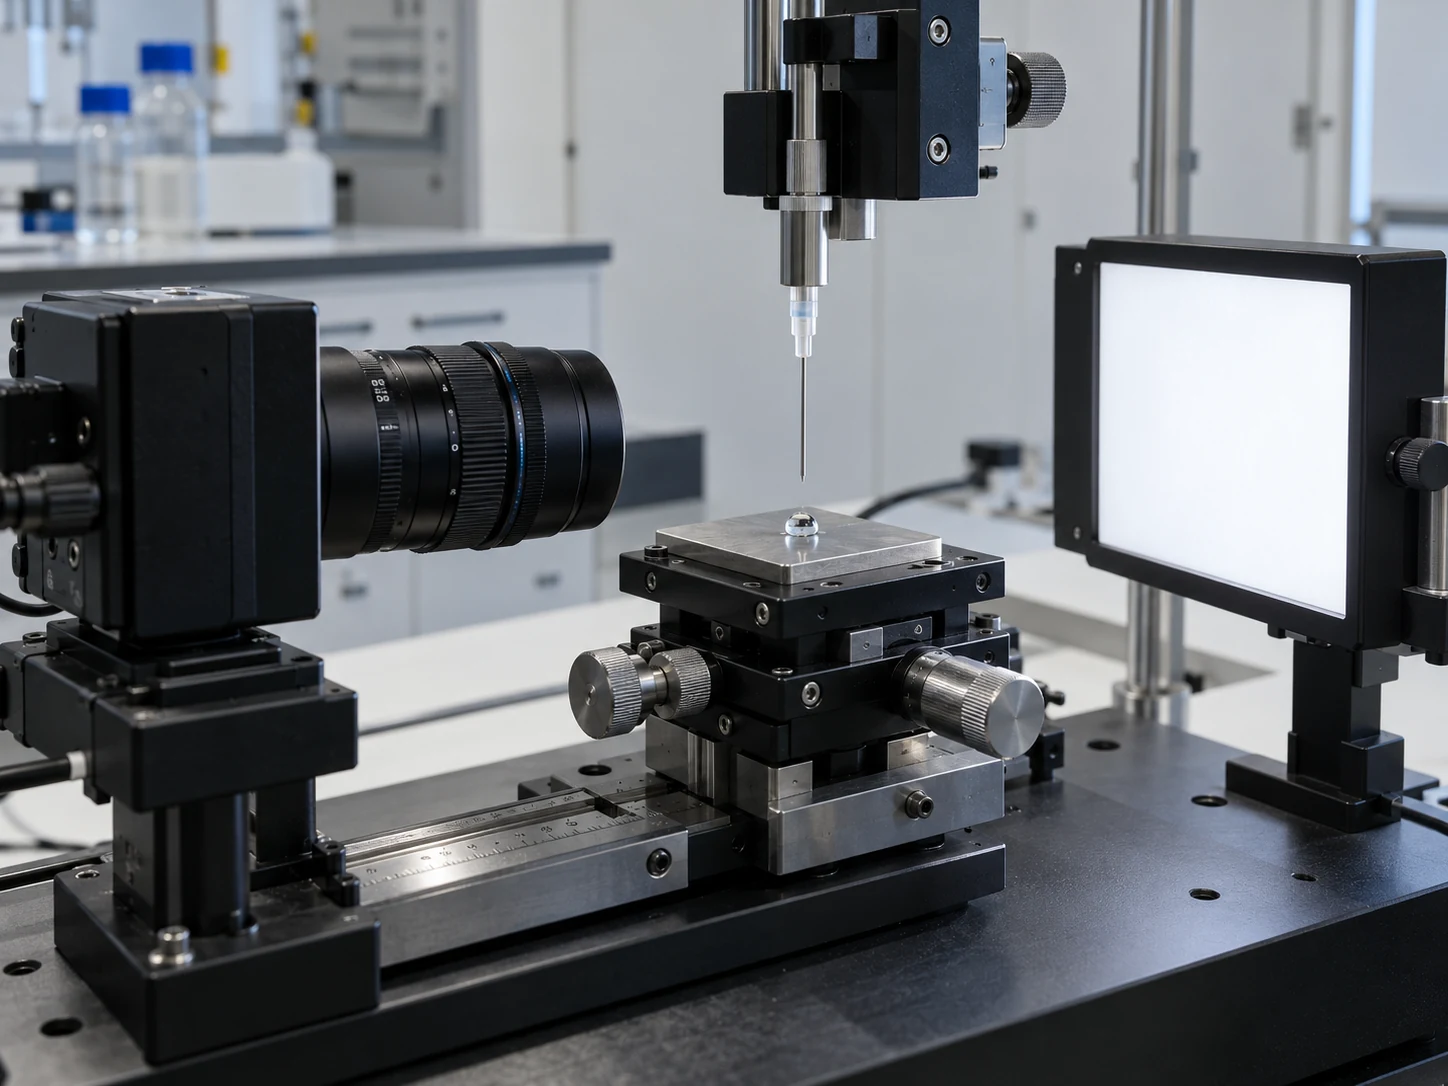
Quantify how readily water wets the finished surface and track whether hydrophobic behavior remains within the required window after wear or environmental exposure
Testing support can include
Available methods can include static or advancing water contact angle using an agreed goniometer method such as ASTM D7334 where applicable, together with retained contact angle after abrasion, cleaning or environmental exposure
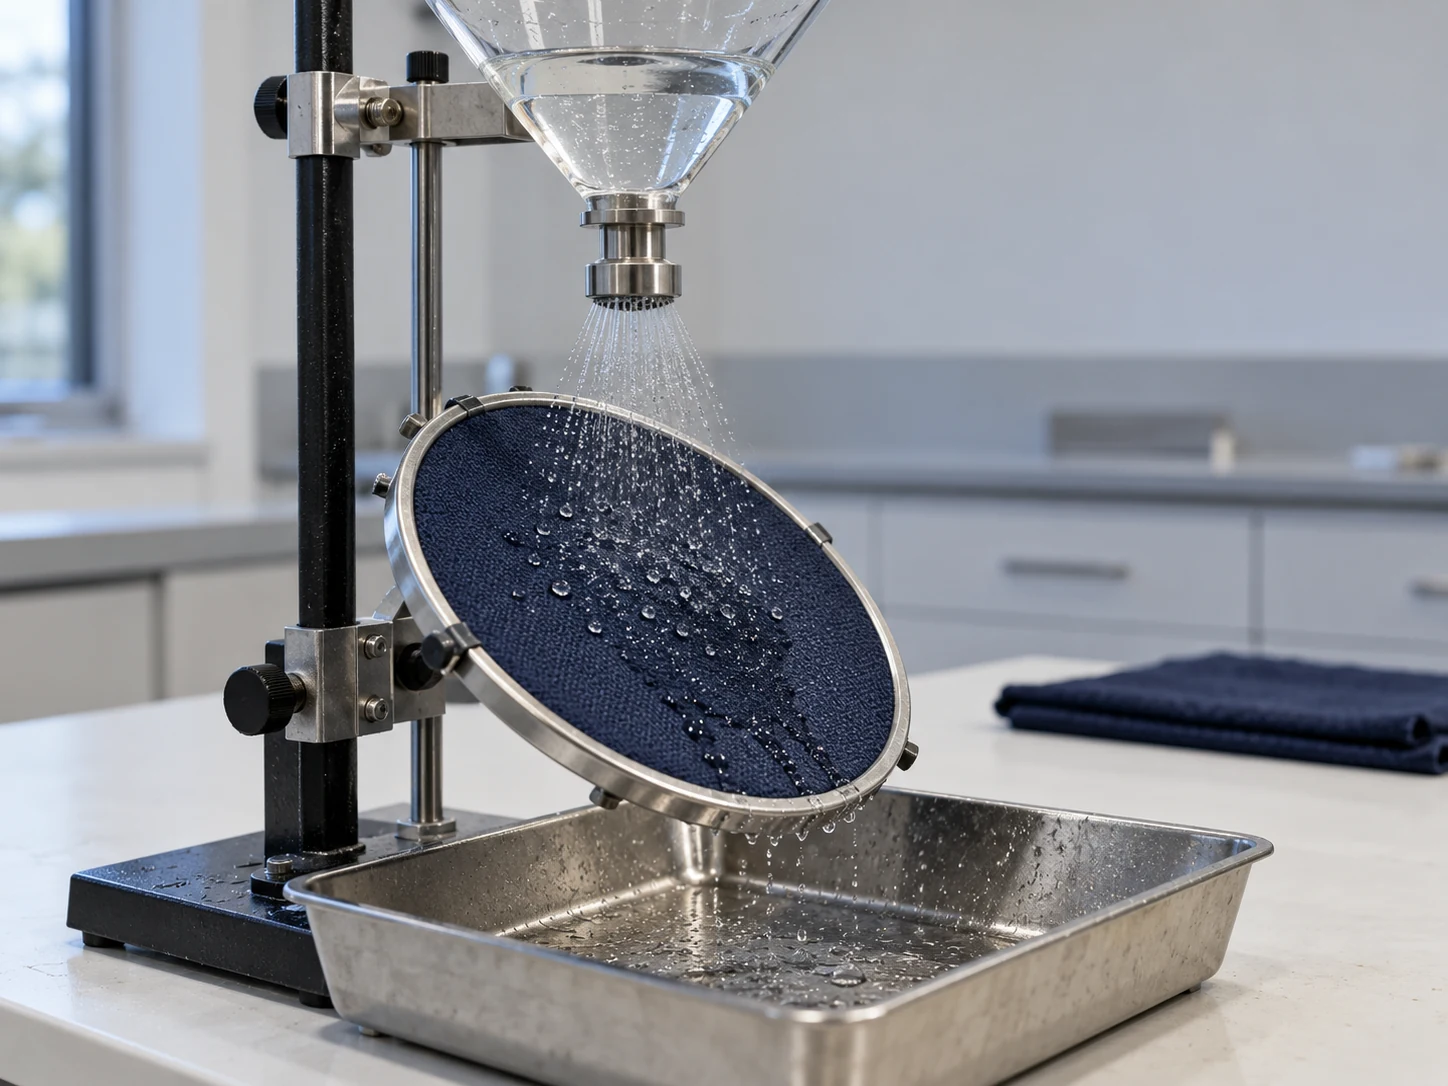
Evaluate how the finished textile or flexible material manages spray, water uptake and penetration so the test result reflects the level of protection the product actually requires
Testing support can include
Available methods can include AATCC TM22 spray repellency, AATCC TM42 impact penetration, AATCC TM127 or ISO 811 hydrostatic pressure, water absorption or moisture retention and air permeability where breathability is part of the product requirement
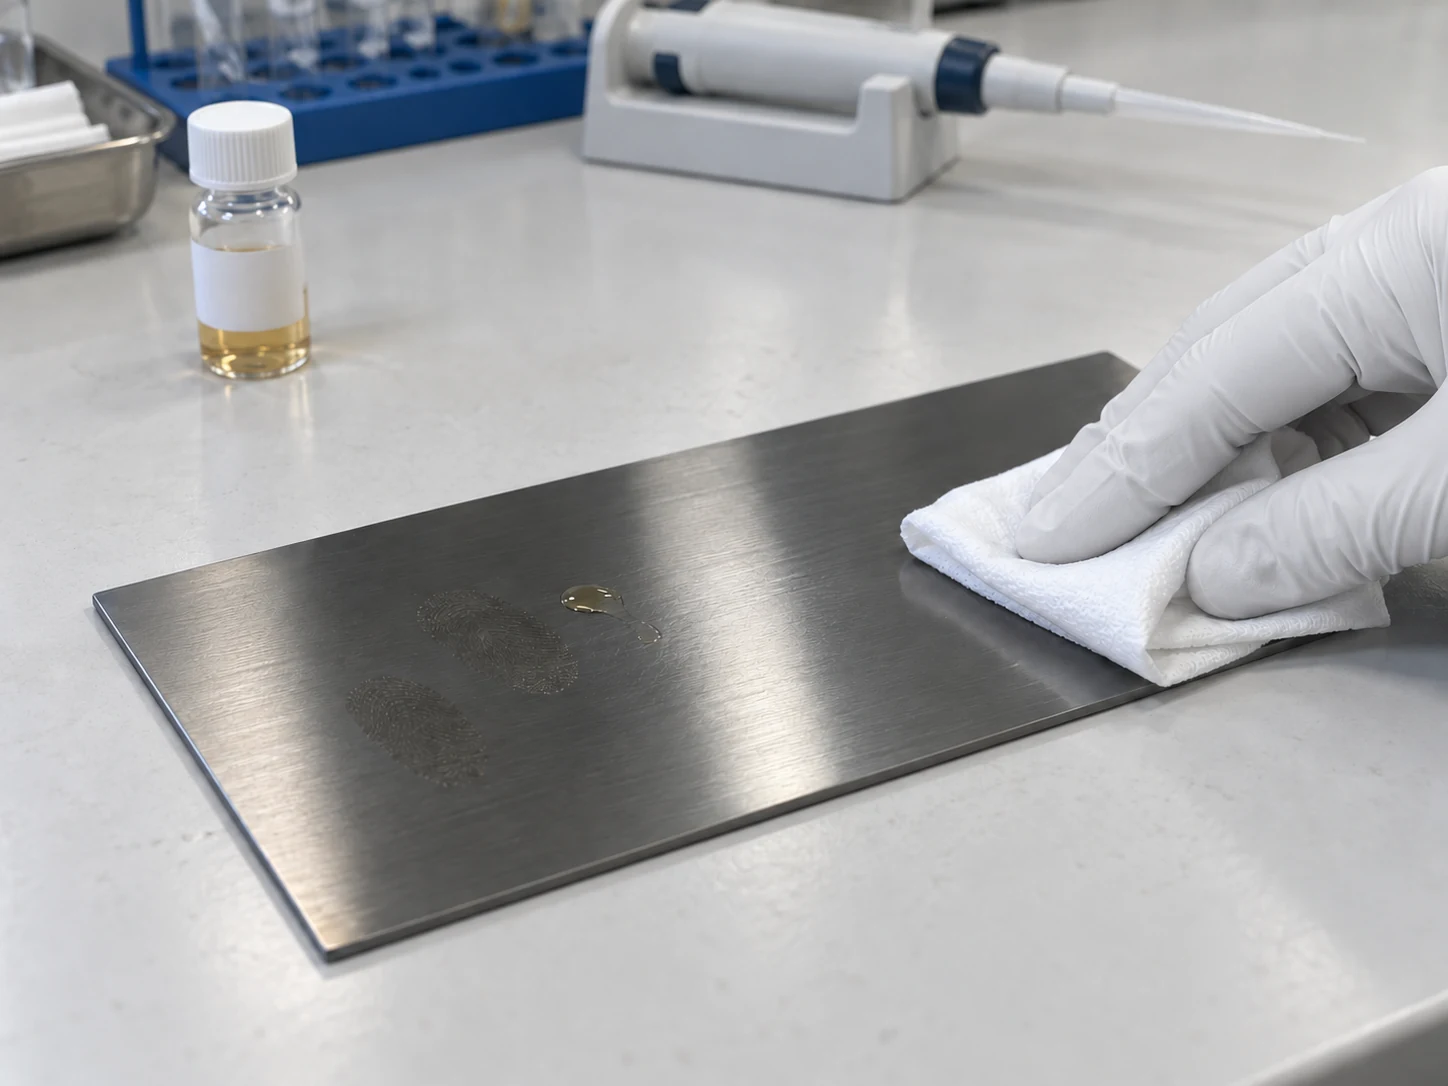
Assess oil and fingerprint behavior with defined contaminants so oleophobic performance can be linked to wipeability, stain release and the way the surface feels through repeated use
Testing support can include
Available methods can include oil contact angle using n hexadecane, mineral oil or agreed artificial sebum, AATCC TM118 for suitable textile applications, controlled sebum transfer, wipe count cleanability and defined coffee or marker stain testing
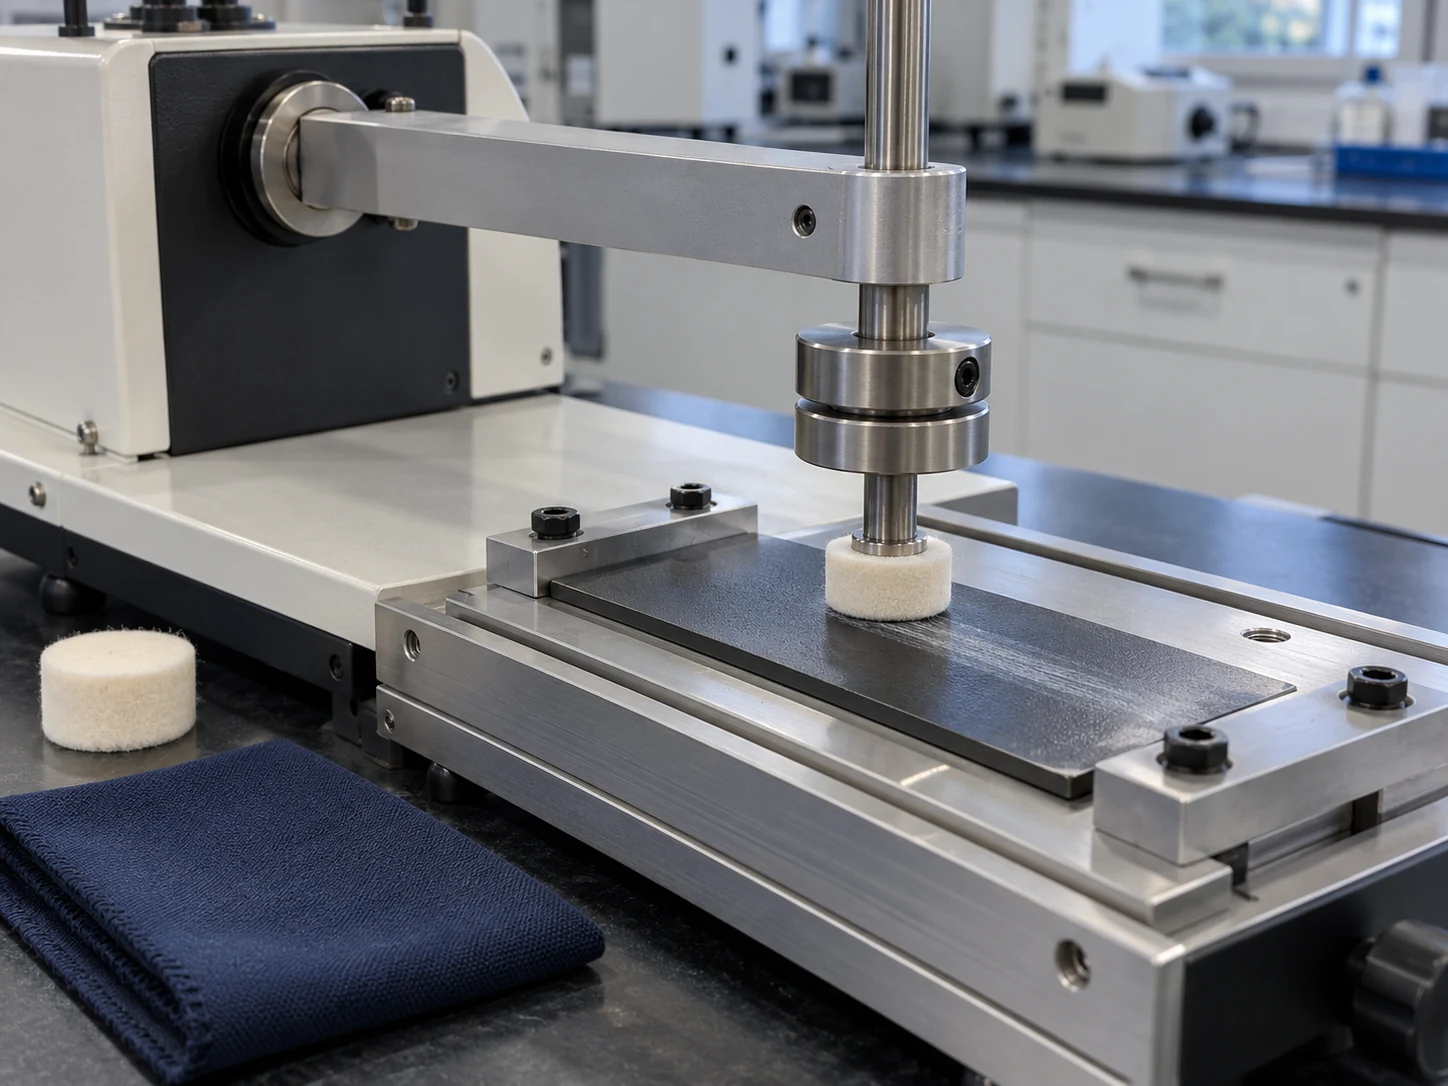
Confirm how much repellency and appearance remain after the product is handled, washed, rubbed or cleaned through the cycles expected in use
Testing support can include
Available methods can include fabric and hard surface abrasion, steel wool and Abrex testing for anti fingerprint surfaces, AATCC TM150 laundering references and customer specific cleaning cycles using the actual detergent or cleaner
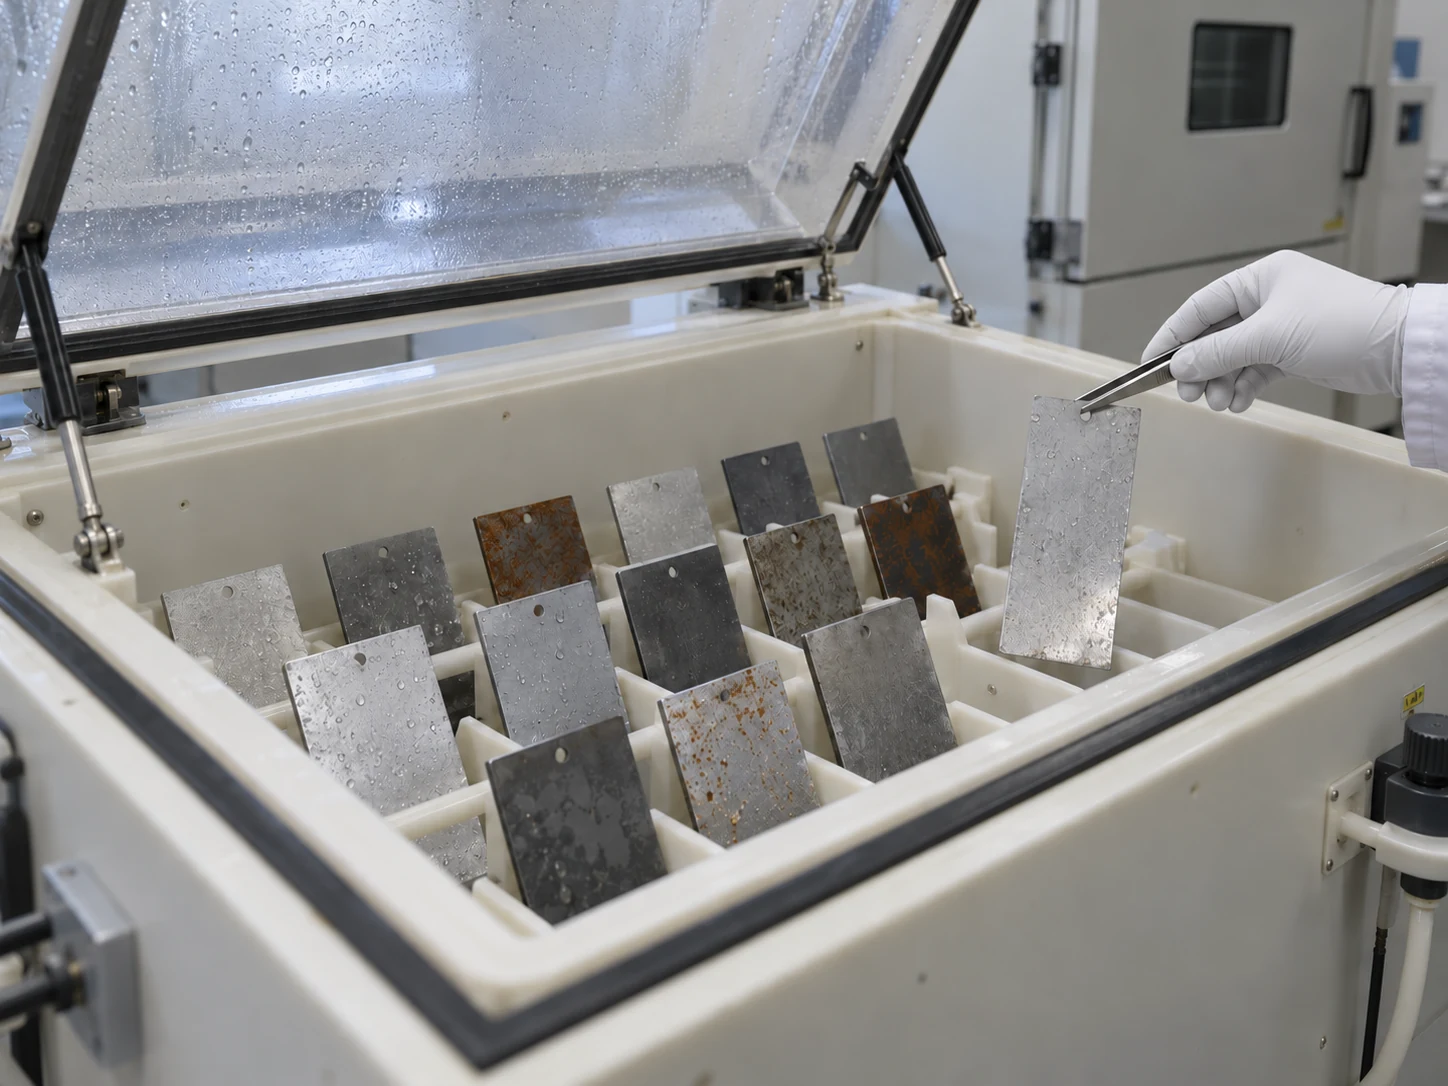
Evaluate how surface protection holds through moisture, salt, sweat, heat and UV so metals and outdoor materials can be reviewed against the environmental conditions that influence service life
Testing support can include
Available methods can include ASTM B117 salt fog where applicable, seawater and artificial sweat exposure, humidity, heat soak, UV weathering and post exposure assessment of wetting, appearance and corrosion
Confirm that repellency and cleanability are achieved without compromising the transparency, haze, color, friction or surface finish expected from displays, glass and premium visible components
Testing support can include
Available methods can include visible transmittance, haze, color shift, gloss, coefficient of friction, tactile evaluation, surface roughness and microscopy selected around the optical or decorative acceptance window
Connect the chemistry requirement with the finished coating result so PFAS-free options can be reviewed together with the material declarations and performance data used for product approval
Testing support can include
Available support can include supplier declarations, targeted PFAS analysis or total fluorine screening through qualified laboratories where required, alongside the repellency, durability and appearance tests used to approve the finished product
NTI Nanofilm provides testing and characterization support for coating development and application qualification. Testing may be performed in house or coordinated through qualified facilities, depending on the site and project scope. Results may reference recognized test methods where applicable and do not constitute independent product certification.
NTI Repel™ brings hydrophobic, oleophobic and electronics protection into industries where water, oils, contamination or moisture can affect product quality, appearance, reliability and service life.
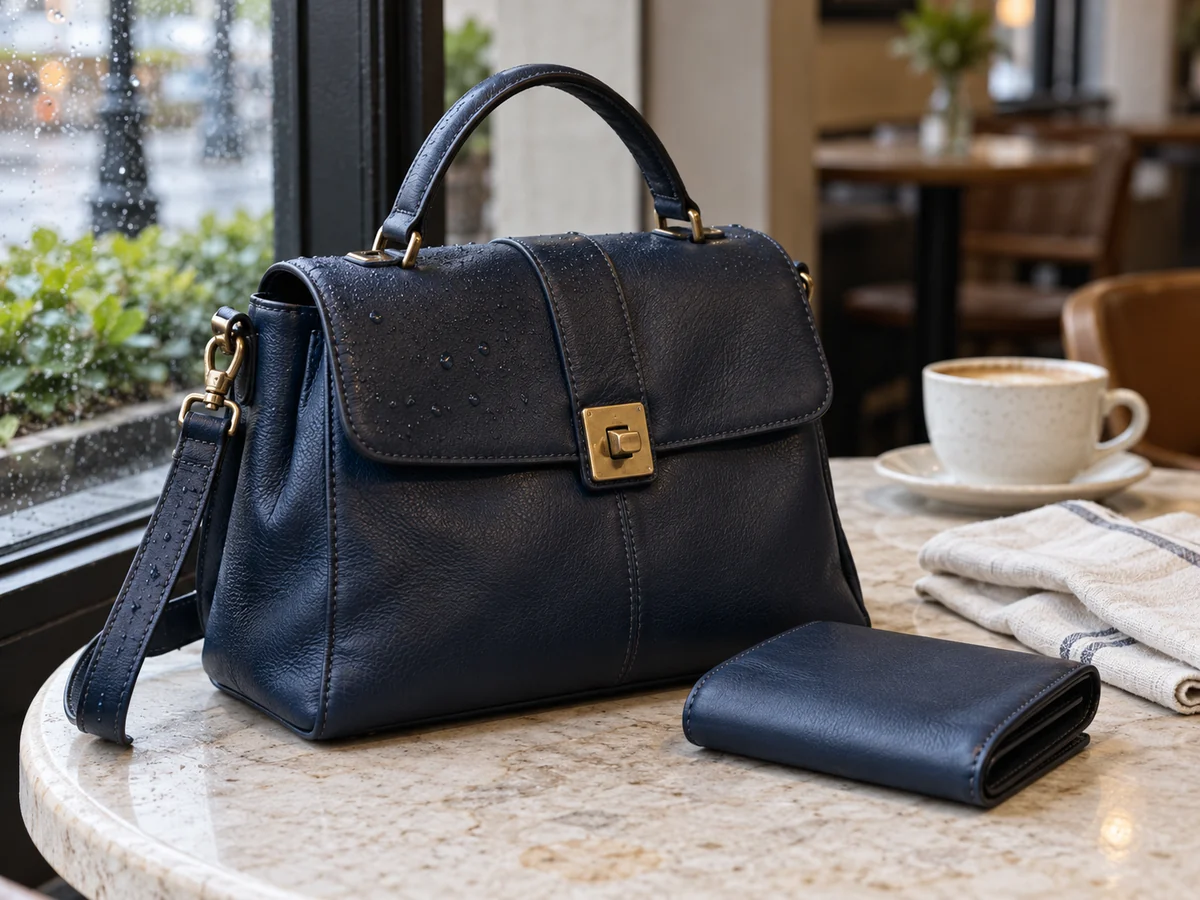
Protect handbags, wallets, straps and premium leather accessories from water and everyday stains while preserving appearance, tactile character and material feel.
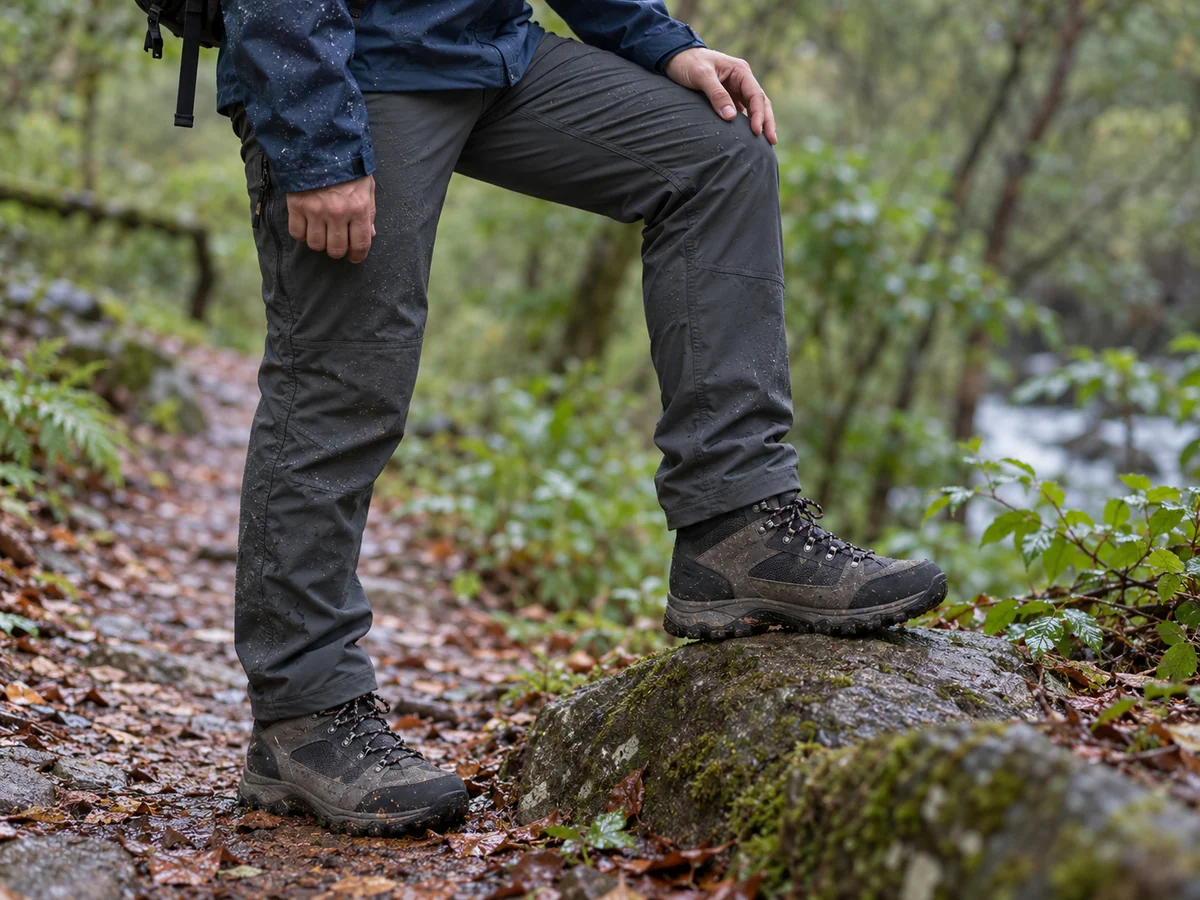
Build water repellency into apparel, footwear, performance fabrics and outdoor goods while balancing wash durability, abrasion, flexibility and breathability.
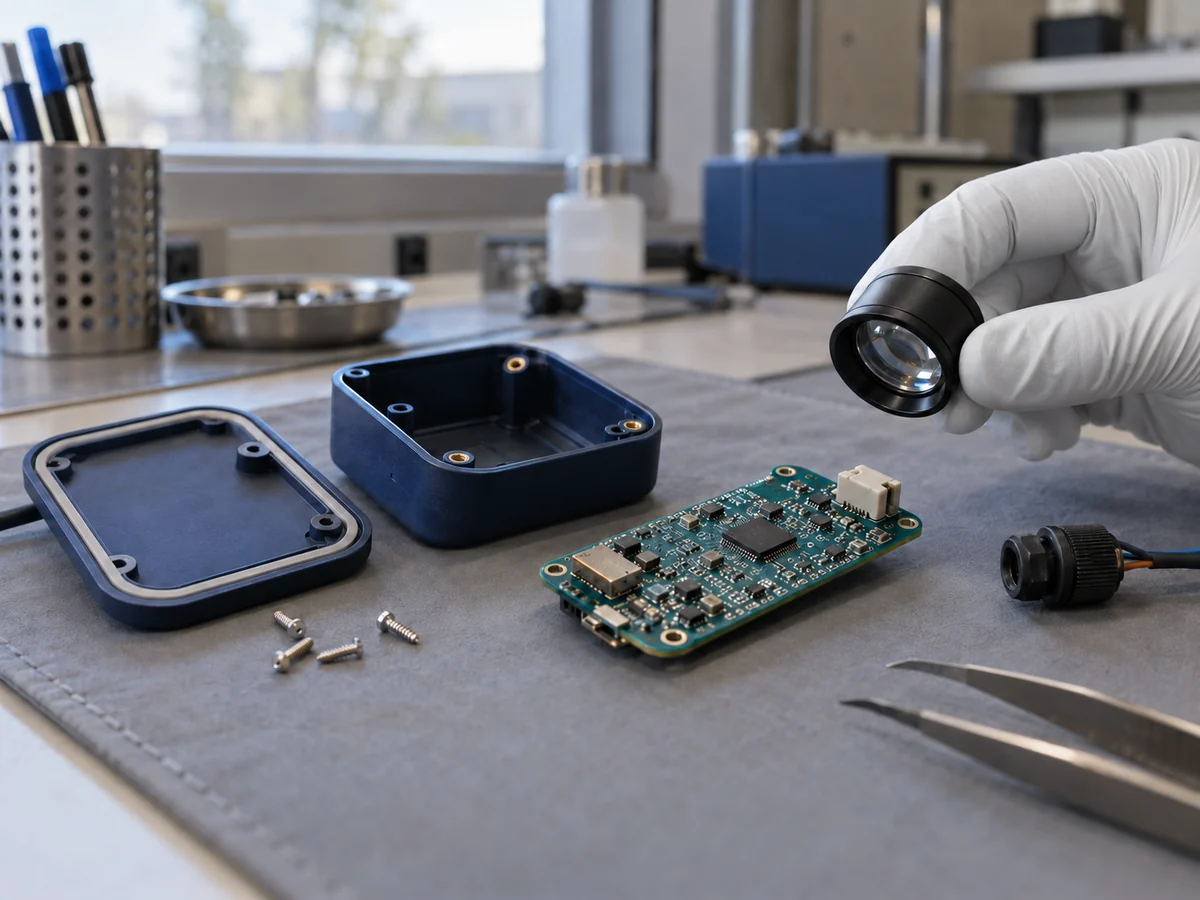
Protect PCBAs, sensors, controls and connected devices from moisture, condensation, salt and liquid exposure while keeping electrical reliability central to qualification.
Support electronic modules, controls, decorative surfaces and exposed components where humidity, salt, fingerprints and repeated handling influence reliability and perceived quality.
Reduce water spots, fingerprints, oily residue and moisture exposure on faucets, fittings, controls and visible hardware where easy cleaning and long term appearance matter.
Control fingerprints, sebum and everyday contamination on pens, watches, controls and decorative metal surfaces where finish quality is part of the product experience.
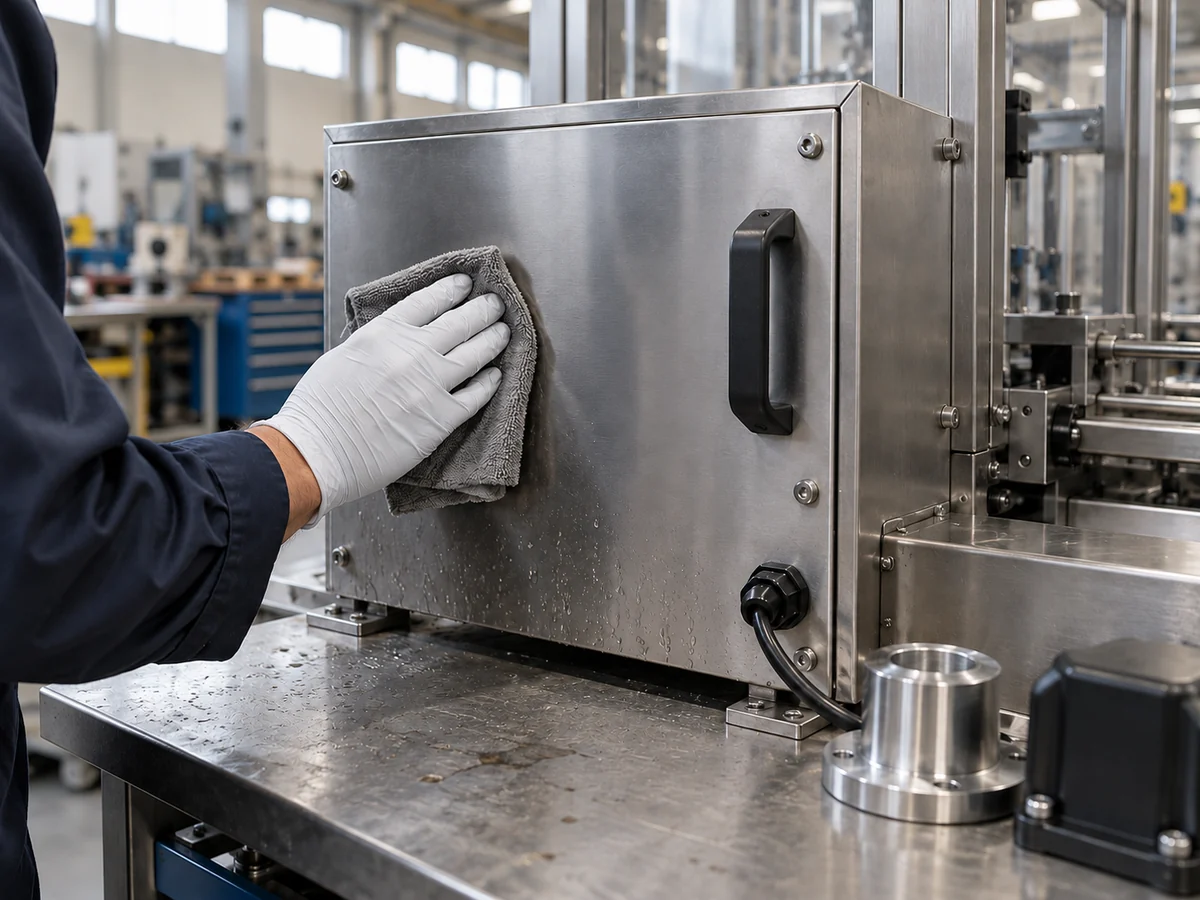
Reduce wetting, contamination and moisture exposure on metal and polymer components that must remain easier to maintain while preserving dimensional and surface requirements.
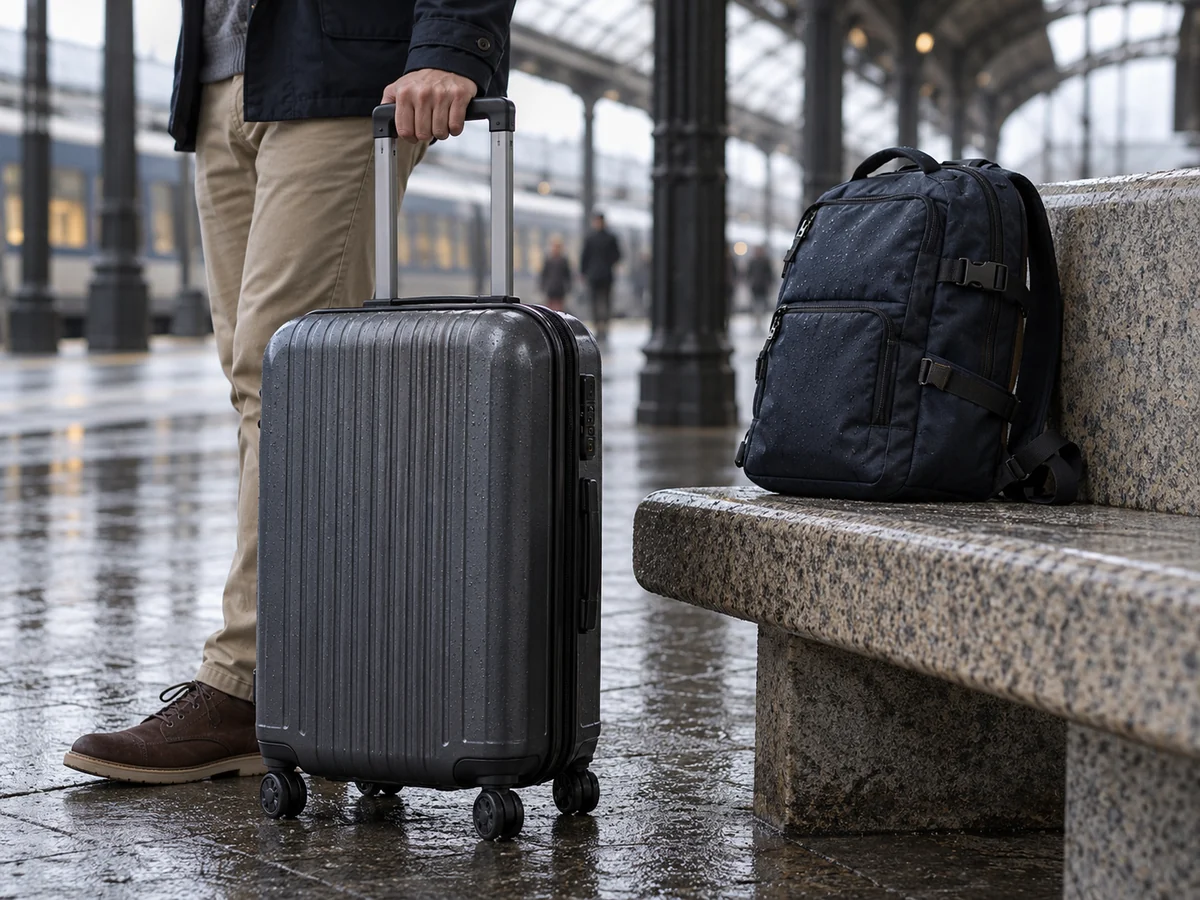
Protect luggage, backpacks and mixed material accessories from rain, spills and grime through repeated travel, handling and cleaning.
Bring us the product and the exposure it has to handle. We work with your team to turn water, oil, stain or moisture requirements into a coated surface that can be measured, qualified and reproduced in production.
Share the water, oil, sweat, salt, stain, cleaning and handling conditions that are affecting appearance, reliability or service life.
We look at the material, finish, geometry, colour, feel, optical needs and any temperature or handling constraints before selecting a coating route.
Hydrophobic, oleophobic, PFAS-free or other application selected chemistry is matched to the performance window your product needs.
Samples are evaluated against the wetting, penetration, abrasion, corrosion, cleaning, optical or tactile conditions that will determine acceptance.
Qualified process settings, fixturing, inspection and acceptance criteria are aligned so the surface performance can be reproduced in ongoing supply.
Explore related technologies, testing insights and coating solutions for water resistance, PFAS-free surfaces, oil release and anti fingerprint performance
Share the surface, what it needs to resist and the performance you need to preserve. NTI can help you identify the most relevant Hydro Repel™, Oleo Repel™ or Electro Repel™ route and move from representative parts toward repeatable coating supply.
A hydrophobic coating reduces how readily water wets a surface, commonly measured through water contact angle or repellency tests. Waterproof performance describes resistance to water penetration through the finished material, assembly or enclosure. A surface can therefore be highly hydrophobic without being waterproof.
Hydrophobic coatings reduce water wetting. Oleophobic coatings reduce wetting and adhesion by oils, sebum and other low surface tension contaminants. Anti fingerprint performance usually combines oil release with easier wiping, lower fingerprint visibility, smooth touch and retained performance after repeated handling.
PFAS requirements are increasingly influencing material selection, supplier qualification and market access. In the EU, Regulation (EU) 2024/2462 introduces PFHxA limits for specified consumer textiles, leather, related accessories and footwear from 10 October 2026. Customer restricted substance lists and certification schemes can introduce additional requirements, which is why PFAS-free alternatives are being considered earlier in product development.
Yes. PFAS-free options are available across NTI Hydro Repel™, NTI Oleo Repel™ and NTI Electro Repel™ routes, subject to material compatibility and application qualification. The selected chemistry is matched to the water repellency, oil release, cleanability, corrosion or electronics protection required by the product.
Plasma Enhanced Chemical Vapor Deposition, or PECVD, is a dry vapor phase coating process that uses plasma to activate precursor chemistry and form a thin functional film directly on the surface. It can create hydrophobic or protective properties without applying a conventional liquid finish to the product.
NTI Advanced PECVD uses a high density plasma environment to provide greater control over precursor activation and thin film formation. The platform uses an inductively coupled plasma source, while many conventional PECVD systems use capacitively coupled plasma. For customers, the practical advantage is greater process control to tune repellency, durability and coating consistency across different materials and applications.
Spray, dip and pad dry cure finishes are widely used and remain suitable for many textile products. PECVD forms the repellent function directly on fibre surfaces through a dry vapor phase process, reducing liquid add on, drying and cure dependence while helping preserve fabric airflow, flexibility and handle.
Yes, when the coating route and fabric construction are properly matched. Ultra thin plasma deposited films can functionalize fibre surfaces without filling the textile structure with a heavy continuous layer, helping retain air permeability, flexibility and hand feel together with water repellency.
NTI Hydro Repel™ is organized into NTI Hydro Soft Repel™ for fabrics, leather and flexible materials, NTI Hydro Polymer Repel™ for selected polymers and composites, and NTI Hydro Metal Repel™ for selected metal surfaces. Compatibility depends on the actual substrate chemistry, finish, additives and geometry.
Yes. PECVD can form ultra thin low surface energy barrier films that reduce water wetting and can support fouling and corrosion resistance on selected metals. Final performance depends on film chemistry, substrate preparation, coating continuity and the actual exposure environment.
Oleophobic performance is commonly evaluated with a defined oil or hydrocarbon liquid, contact angle, sliding behavior or cleanability method. Anti fingerprint evaluation can also include artificial sebum, fingerprint visibility, wipeability, surface appearance, touch friction and durability after repeated cleaning or abrasion.
NTI Electro PCBA Repel™ is a dry thin film conformal coating alternative for PCBA moisture, liquid and corrosion protection. It is designed for electronic assemblies exposed to humidity, condensation, salt or liquid conditions where corrosion resistance and electrical reliability are important.
Conventional liquid conformal coatings commonly use acrylic, polyurethane, silicone or epoxy chemistries, while Parylene is deposited by chemical vapor deposition. IPC describes conventional conformal coatings as typically 12.5 to 200 μm thick, while representative PECVD PCBA protection has been demonstrated at 0.25 to 0.30 μm. This ultra thin route can be attractive where moisture and corrosion protection must be balanced with form factor, heat transfer or high frequency electrical performance.
No coating by itself establishes an enclosure IP rating. IPX7 and IPX8 are ratings for the finished enclosure or device under IEC 60529. NTI Electro PCBA Repel™ can be evaluated for moisture or immersion protection at assembly level, while any final IP rating must be validated on the complete product.
Yes. Products can combine different materials and surface requirements. A high touch metal assembly, for example, may need hydrophobic moisture protection together with anti fingerprint and easy clean performance. The NTI Repel™ Solution Finder can return two relevant routes when the selected challenge and construction indicate complementary surface functions.
The finder uses two customer inputs: what the surface or assembly needs protection from, and what material or assembly is being protected. Those two inputs are enough to identify the most relevant starting route in most cases without asking users to define detailed laboratory tests before the coating direction is known.
NTI Nanofilm can support coating development and application qualification across surface wetting, water repellency and penetration, oil and sebum release, abrasion and wash durability, corrosion and environmental exposure, optical and tactile performance, electrical reliability and chemistry verification. Testing may be performed in house or coordinated through qualified facilities depending on site and project scope.